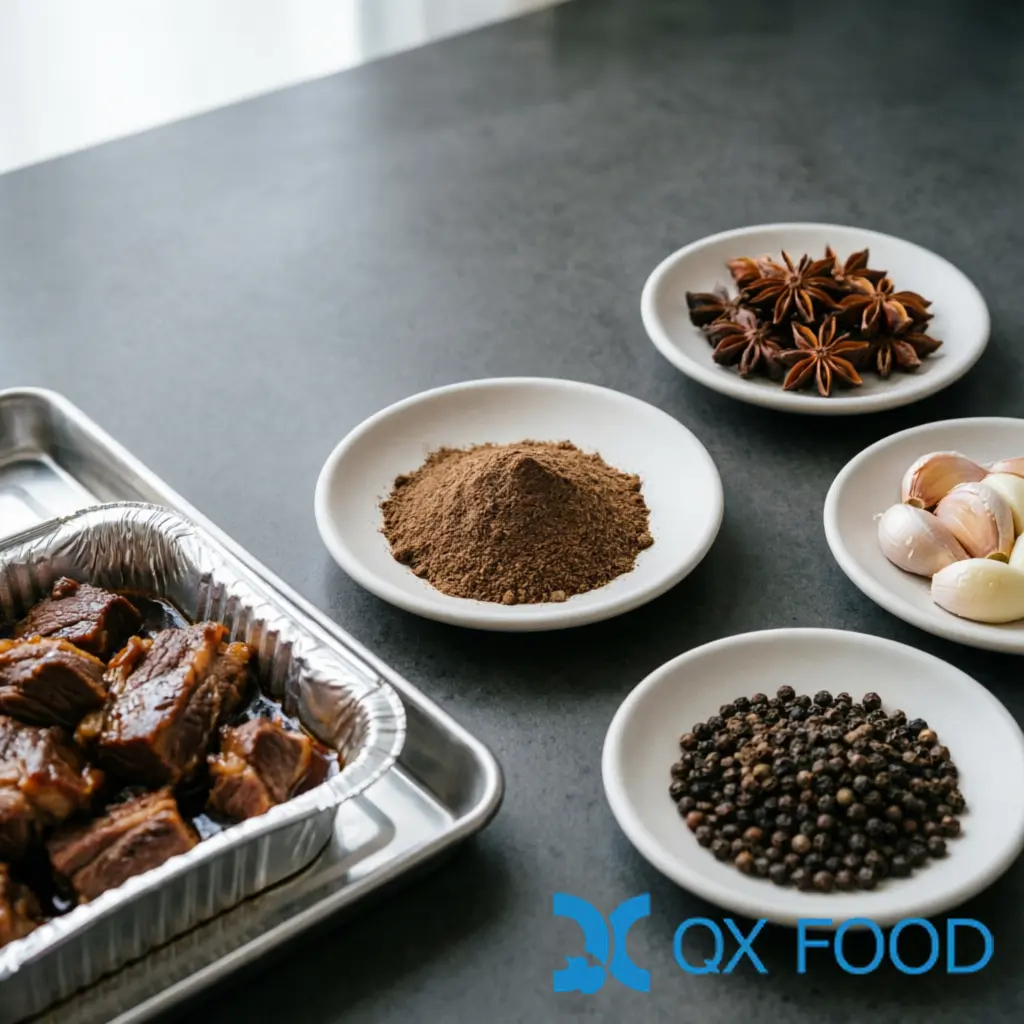
Ready meal ingredients that perform in a bench kitchen can fail after transfer to a production line even when the ingredient list appears unchanged. Heating, mixing, dosing, cooling, packaging and ingredient variability all change with scale. Scale-up therefore requires more than multiplying a recipe: the formulation, process and supplier controls have to be validated together.
Quick answer. A ready-meal ingredient is not commercially approved because one sample tastes right. Qualification moves through linked stages: product-specific specification, bench or pilot process testing, supplier qualification and commercial-line validation. Formula ratios can be a starting point, but heat transfer, mixing, dosing, cooling and package or process interactions change with scale, so the finished product must be revalidated under production-relevant conditions.
Ready Meal Scale-Up Is a Formula + Process Transfer Problem
Two statements sound similar and mean different things. Formula scaling multiplies ingredient quantities from a bench recipe to a commercial batch size. Process scaling transfers the formulation into a different physical system: larger kettles, different heat transfer, longer residence, production dosing and filling equipment. The scaling guidance from University of Maryland Extension is explicit that a recipe has to be converted into a workable, repeatable production formula and that several scale-up attempts are normal.
Mass-based formula ratios are a valid starting point for a commercial batch. What does not scale linearly is the process: mixing behavior, heat transfer, evaporation, shear, residence time and dosing accuracy all change with equipment size and line speed, so the commercial formula may require adjustment after pilot validation. Treat every scale change as a new engineering question, not as arithmetic.
Stage 1: Define the Product and the Ingredient Specification
Define the finished product before requesting ingredients: reference formula, target serving, packaging format and storage type (ambient, chilled or frozen) decide which ingredients and parameters matter. The product definition also decides the specification discipline: shelf-stable retort, chilled sauce and frozen meal place different demands on the same ingredient category.
Sample requests should then identify the grade and the parameters that matter to its intended function. These may include composition, particle characteristics, moisture, color, pungency, salt, acidity, microbiological limits or other analytical markers where the selected ingredient controls them. Do not apply one fixed specification template across ready meal ingredients. A garlic powder specification may center on particle size, moisture and microbiological limits; an HVP grade on salt, nitrogen and moisture; a soy sauce powder on salt, composition and moisture; a tomato ingredient on color, acidity and composition. The SKU determines the specification, not the category template.
For a production-grade sample, request the applicable specification and the available batch or sample documentation. The buyer should know which parameters are specification targets, which are batch-tested, and which belong in supporting technical documentation before approving the commercial grade. Moisture or water-related parameters should be compared where they are controlled for the grade, particularly when flow, caking or storage behavior matters.
Stage 2: Identify the Product-Specific Critical Quality Attributes
Measure the attributes that define success for the specific product rather than one universal panel. For a sauce, viscosity, solids and color may define the product; for a rice or noodle meal, moisture, texture and yield; for a retort stew, viscosity, particulate integrity and the thermal critical factors of the scheduled process; for a chilled sauce, pH, water activity, cooling and sensory performance where applicable. These product-specific critical quality attributes (CQAs) become the acceptance language for ready meal ingredients at every stage, because bench, pilot and commercial runs can only be compared when everyone measures the same endpoints.
Stage 3: Bench and Pilot Testing Against Production-Relevant Conditions
Bench and pilot trials should reproduce the production-relevant process history as closely as practical: heating rate, peak temperature, hold time, mixing or shear, evaporation, filling and cooling. Equipment does not have to be identical, but the critical process conditions and their effect on the product must be understood. Where a bench trial cannot reach production heat input, document the difference and test its effect on the finished product.
For the sauce and seasoning layer of ready meals, the prepared meal sauce pack development guide details how the thermal process shapes flavor formulation, and the same discipline applies to every ingredient in the pack.
Thermal Safety Validation Is Separate From Formulation Testing
For shelf-stable foods in hermetically sealed containers, formulation testing must not be confused with process-safety validation. The safety process is product-, package- and equipment-specific. For products intended for the United States, first determine whether the product falls under FDA’s low-acid canned food (LACF) or acidified-food requirements: LACF is any food with finished equilibrium pH above 4.6 and water activity above 0.85, and an acidified food is a low-acid food acidified to a finished equilibrium pH of 4.6 or below with water activity above 0.85. Commercial processors subject to those rules must register the establishment and file the applicable scheduled process for each product, product style, container size and type and processing method (21 CFR 108), as summarized in the FDA acidified and low-acid canned foods guidance index. Changes to viscosity, particle size, fill weight or formulation can affect heat penetration and may require process review under the LACF establishment registration and process filing rules. In practice this means ingredient selection must stay inside the validated process window, and any ingredient change that moves a critical factor may require review by the competent processing authority or another appropriately qualified process expert before commercial production.
Stage 4: Qualify the Supplier Before Commercial Approval
Sample approval qualifies the ingredient; supplier qualification qualifies the supply. Apply the same structure used across this site: pass-or-fail qualification gates first, then commercial and technical evidence. Gates cover food safety and legal compliance, allergen control, traceability, destination-market requirements and the applicable certification scope for the product. Evidence includes the product specification, batch COA, technical documentation, capacity and lead times, and change control. HACCP is a hazard-analysis methodology rather than one globally uniform certificate, and certification scope should be checked for the SKU and market in question. The full gate-plus-evidence method is laid out in our snack seasoning supplier evaluation guide.
Stage 5: Validate Dosing, Mixing and Line Handling
Ingredients that behaved in a 5 kg trial can fail at production rate through dosing inaccuracy, segregation, bridging or poor mixing. Verify dosing accuracy and powder handling at production rate. If feeding or flow fails, identify whether the cause is particle characteristics, bulk density, consolidation, caking, segregation, feeder design or formulation before changing the ingredient specification. The powder caking prevention guide covers the system behavior behind flow failures; changing mesh or adding a flow agent without diagnosis can create a label and specification problem instead of solving the line problem.
Stage 6: Commercial Run and Multiple-Lot Follow-Up
The first commercial run validates the transfer: full batch size, line conditions, the agreed CQAs and the specification. After the first production run, evaluate multiple independent commercial lots where appropriate to confirm that the process remains within the pre-defined product specification and application standard. Three lots may be a practical initial exercise, but it is not a universal validation requirement. Multiple-lot data also should not be used by itself to create specification limits; specification ranges come from product design, process capability, regulatory and customer requirements and validated application needs.
The literature on prepared dishes makes the same structural point: quantification and standardization are the defining features of central-kitchen and ready-meal engineering, as documented in a central kitchen engineering review in Trends in Food Science & Technology. The craft-to-quantified transition is exactly what the stages above formalize.
Build the Ingredient Shortlist by Function, Not by a Universal Workhorse Set
Ready meals are too broad for one universal ingredient set: an Asian rice bowl, a pasta dish, a curry, a frozen meal, a retort stew and a chilled sauce do not share one shortlist, so ready meal ingredients should be selected around product function, process, label and market requirements. Start from the finished-product target and work backward:
| Function | Ingredient types to evaluate |
|---|---|
| Savory base | HVP, fermented powders, yeast-derived ingredients |
| Aromatic layer | Garlic, onion, ginger, spices |
| Heat or pungency | Chili, pepper, regional spice systems |
| Color | Tomato, paprika or other appropriate color-contributing ingredients |
| Texture or body | Starch, hydrocolloid or solids system |
| Acid, salt and sweet balance | Product-specific |
| Signature identity | Regional or brand-specific ingredients |
Each candidate ingredient on the shortlist then passes through the same stages: product-specific specification, CQAs, process testing, supplier gates and line validation.
QXFOOD Ingredient Families for Ready-Meal Trials
QXFOOD supplies ingredient families that support ready-meal trials, published as separate products with their own specifications rather than as one prescribed combination:
- Savory base: soy sauce powder and hydrolyzed soy protein.
- Aromatic layer: garlic powder and ginger.
- Heat: black pepper and white pepper powders.
- Signature identity: star anise, cassia, fennel and clove.
For the full category view, visit the raw spices and herbs category page.
Specification, Batch COA and Technical Documentation
Three document layers answer different questions. The product specification defines the grade: controlled parameters, limits and the acceptance basis. The batch COA reports the actual measured results required by the SKU specification for a specific lot. Technical documentation carries supporting detail such as the analytical methods used for controlled parameters, process description and application guidance. For ready meal ingredients, the supplier should define the analytical methods for controlled parameters, while the batch COA reports the actual results required by the specification; methods do not have to be repeated on every COA line.
How QXFOOD Supports Ready-Meal Scale-Up
QXFOOD can support ready-meal ingredient trials with product-specific specifications, applicable batch documentation, samples and technical or certification documentation for the selected SKU. Available sample quantity, analytical parameters, certification scope and application-support level should be confirmed for the selected product and project rather than assumed from a category description.
Download the Ready Meal Scale-Up Qualification Checklist to run the same stages across your product, ingredients, process, suppliers and commercial runs.
Ready Meal Scale-Up Qualification Checklist
Product definition · ingredient specification · CQAs · process transfer · supplier approval · commercial run. Track every scale-up stage in one two-page worksheet.
Request ready meal ingredient samples through the contact form on this page, and the application team will support your qualification program.
Frequently Asked Questions
Why do ready meal ingredients fail at production scale?
Dosing variance, heat-load differences, ingredient variability and cost-structure shifts all appear between the lab and the line. The sample is the first data point of a qualification program, not the decision itself.
What should a ready meal ingredient sample request include?
The product definition, the grade, and the parameters that matter to the ingredient’s intended function: composition, particle characteristics, moisture, color, pungency, salt, acidity or microbiological limits where the selected ingredient controls them. Do not apply one fixed specification template to every ingredient, and request the applicable specification and available batch documentation rather than assuming every sample carries a full measured COA.
How do I test ready meal ingredients at bench and pilot scale?
Reproduce the production-relevant process history as closely as practical: heating rate, peak temperature, hold time, mixing or shear, evaporation, filling and cooling. Equipment does not have to be identical, but the critical process conditions and their effect on the product must be understood, and the product-specific CQAs must be measured at every stage.
Do ingredient amounts scale proportionately?
Mass-based formula ratios are a valid starting point for a commercial batch. What does not scale linearly is the process: mixing, heat transfer, evaporation, shear, residence time and dosing accuracy change with equipment and line speed, so the commercial formula may require adjustment after pilot validation. Several scale-up iterations are normal.
How do I build an ingredient shortlist for a ready meal?
Start from the finished-product target and select by function, process, label and market requirements: savory base, aromatic layer, heat, color, texture, acid-salt-sweet balance and signature identity. There is no universal workhorse set for all ready meals.
How is retort formulation testing different from scheduled-process validation?
Formulation testing develops the product; scheduled-process validation establishes the safe thermal process for a specific product, container and equipment. For low-acid or acidified foods sold in the United States, FDA requires establishment registration and scheduled-process filing (21 CFR 108), and ingredient changes that affect viscosity, particle size, fill weight or formulation may require process review.
What does supplier qualification cover for ready-meal ingredients?
Qualification gates first: food safety and legal compliance, allergen control, traceability, destination-market requirements and applicable certification scope. Then evidence: product specification, batch COA, technical documentation, capacity and lead times, and change control.